Reverse engineering mining spare parts
The part that stops the plant is the one nobody makes any more: an OEM long since gone, a drawing that was never supplied, a component modified on site until it matches nothing. Re-making it starts with measuring the worn original by hand and hoping the wear is symmetrical.
Scanned at 0.1 mm, the worn part is rebuilt as a CAD model with the wear taken out, made, and the new part verified against the scan before it ships — Element holds under 0.1 mm per 1000 mm of diameter on crusher parts this way.

How are mining spare parts reverse engineered from a 3D scan?
The worn part is scanned at 0.1 mm, rebuilt as CAD with wear corrected, manufactured, then scanned again and compared with the model before it ships.
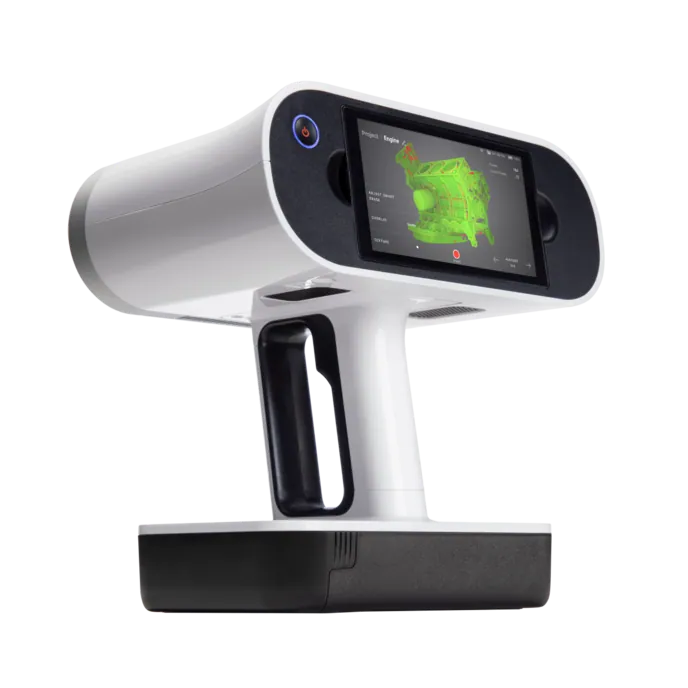
0.1 mm on the partLeo records the worn original at 0.1 mm with 2.3 MP colour, wirelessly.
A model the shop can makeScan to CAD in Geomagic Design X, with wear corrected and features rebuilt.
Verified before shippingThe finished part scanned and compared to CAD — 4 hours from scan to deviation report.
A drawing at lastThe obsolete part has a CAD model and a drawing for the next time.
Why the obsolete part is measured with callipers
When a part has no drawing — the OEM is gone, the plant was bought second-hand, the component was modified on site — the only source of its geometry is the worn one that came out. It is measured with callipers and a tape, the wear is guessed back to a nominal dimension, and a drawing is produced that is partly measurement and partly inference. The new part is made from that drawing, and whether it fits is found out when it is fitted, often on a component large enough that shipping it back is the expensive part.
Element, who manufacture spare parts for mining and construction, described the stakes for a cone crusher mantle: one that does not seat correctly means shipping a very large component back. Their answer was to make measurement the first and last step of the job rather than a guess in the middle.
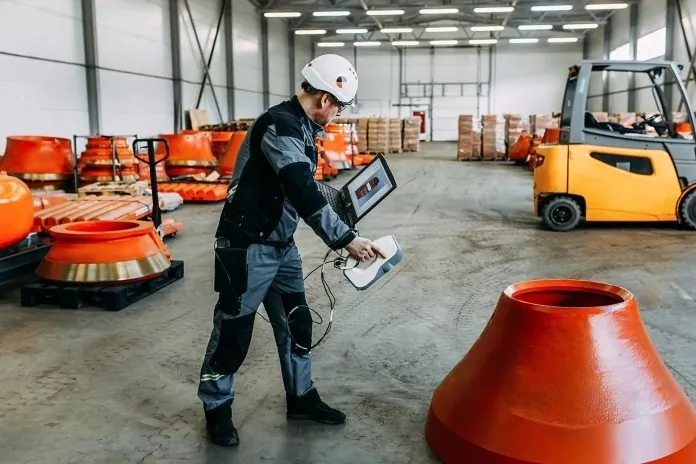
Scanning gives the part a model. Artec Leo records the worn original at 0.1 mm with colour texture, handheld and wireless, in minutes; in Artec Studio and Geomagic Design X the scan is rebuilt as parametric CAD with the wear corrected and the features — bores, keyways, mating faces — reconstructed as they were designed. The part is manufactured from that model and, before it ships, scanned again and compared: Element goes from scan to deviation report inside four hours, as little as 30 minutes on some jobs, holding under 0.1 mm per 1000 mm of diameter to ISO 9001.
From worn original to verified spare
Measurement is the first step and the last.
1. Scan the originalLeo records the worn part at 0.1 mm with colour texture in minutes, wirelessly, on the shop floor or on site.
2. ProcessArtec Studio fuses the scan into a clean, watertight mesh of the part as it is.
3. Rebuild in CADGeomagic Design X rebuilds the part as parametric CAD, correcting wear and reconstructing features to design intent.
4. Make itThe CAD model to the shop — machined, cast or fabricated — with a drawing the part never had.
5. Verify before shippingThe finished part scanned and compared to CAD; the deviation report signed off before it leaves.
Which scanner for this work
Reverse engineering lives or dies on the accuracy of the first scan, which is the handheld scanner’s job; large parts add the tripod scanner for the overall form.

Artec Leo
- Best for
- The part itself — bores, faces, keyways and wear surfaces at 0.1 mm
- Type
- Wireless handheld structured light, all-in-one
- 3D point accuracy, up to
- 0.1 mm
- 3D resolution, up to
- 0.2 mm
- Working distance
- 0.35–1.2 m
- Capture speed
- Up to 35,000,000 points/s in HD Mode
- Onboard
- 5.5″ touchscreen, processing and 512 GB — no laptop
Leo records a component at 0.1 mm with 0.2 mm resolution and 2.3 MP colour, at up to 35 million points per second in HD Mode, which handles dark, wet and reflective metal. Wireless with its screen and processing onboard, it captures a part on a pallet or still on the machine. Element’s scanning engineer worked independently after two days of supervised practice.

Artec Ray II
- Best for
- Very large parts — a mill shell segment, a crusher frame — for the overall form
- Type
- Stationary long-range laser, tripod mounted
- Accuracy, up to
- 1.9 mm at 10 m, 2.9 mm at 20 m, 5.3 mm at 40 m
- Range noise
- 0.4 mm at 10 m
- Range
- 0.5–130 m
- Scan time
- 1 min 42 s at 3 mm, 10 m, without texture
- Field of view
- 360° × 300°
Where the part is metres across, Ray II records the overall form from a tripod at 1.9 mm at 10 m and Leo adds the mating faces at 0.1 mm; both register in Artec Studio. The combination is what 4C used to model a whole excavator with the detail where the analysis needed it.
Done on real parts

“Using Artec 3D scanning for quality control allows you to guarantee the customer a high quality of delivered products as well as minimize logistic costs that would’ve been incurred when returning large equipment.”
See an obsolete part scanned, rebuilt as CAD with the wear taken out, and the new one verified against the model before it ships — book a demo for your maintenance and workshop teams.
Book a demoQuestions maintenance and workshop teams ask
How accurate is the reverse-engineered part?
The scan is 0.1 mm; the CAD rebuild corrects wear to design intent. Element verifies finished crusher parts against the model and holds under 0.1 mm per 1000 mm of diameter to ISO 9001.
Can the wear be taken out of a worn original?
Yes. In Geomagic Design X the surfaces are rebuilt as geometric features — cylinders, planes, cones — fitted to the unworn regions, so the model represents the part as designed rather than as it came out.
What about a part that is still on the machine?
Leo is handheld and wireless, so it records the part in place — a mounting face, a worn bore — without removing it. The CAD rebuild proceeds the same way.
How is the new part verified?
It is scanned and compared with the CAD model in Artec Studio or Geomagic; the deviation report shows every surface against tolerance. Element does this inside four hours, and in as little as 30 minutes on some jobs.
Related applications

Tell us about the parts you cannot source
Describe the part, its size and what documentation exists. A mining specialist will come back with how it would be scanned, rebuilt and verified, and what accuracy the new part would carry.